

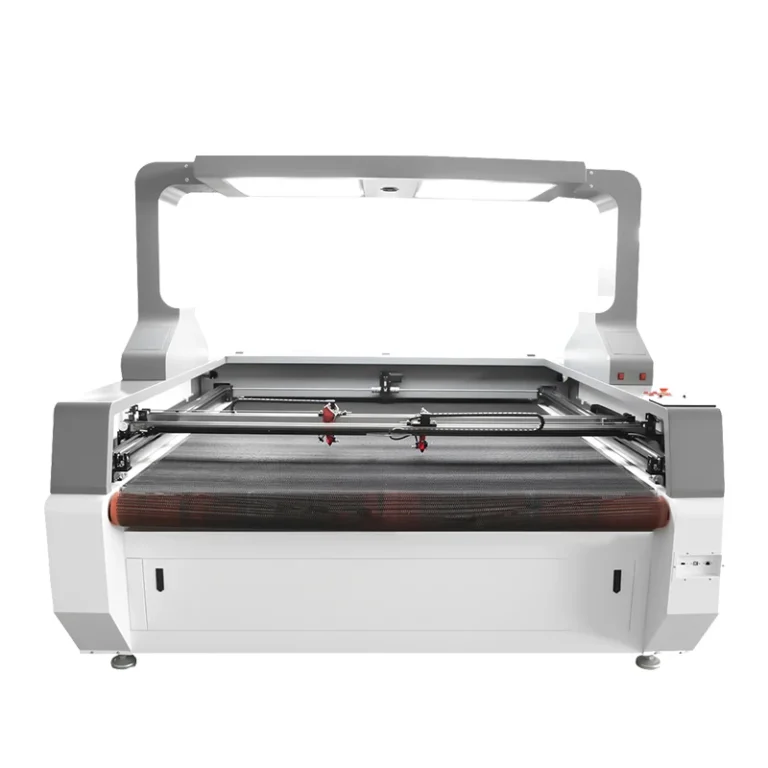
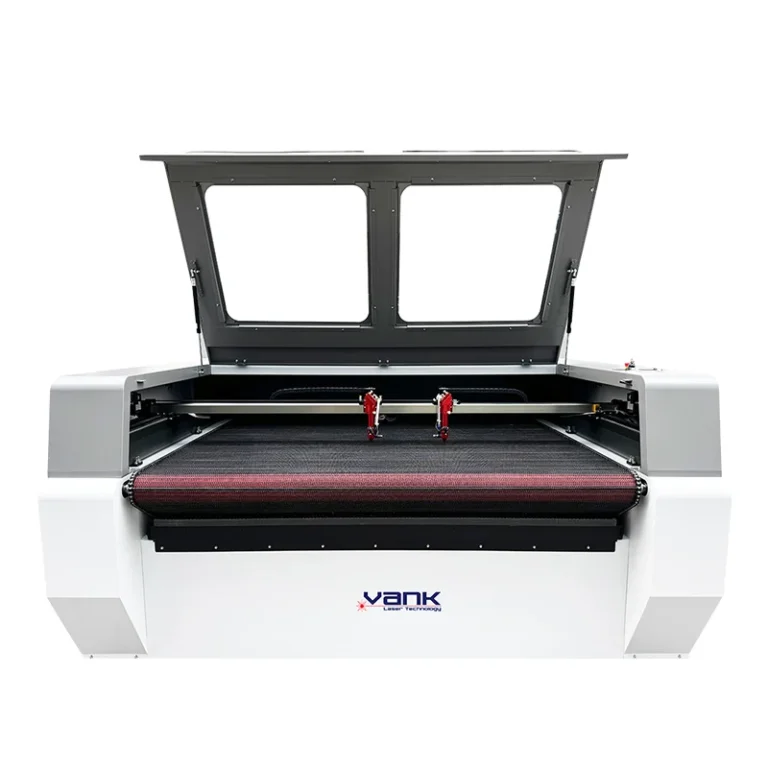
Application and model selection
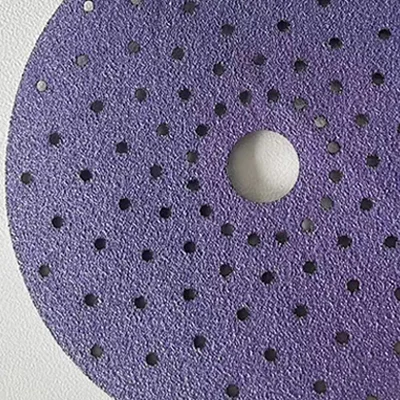
The brochure specifies a TL5269 multi-head controller and shows a camera option. Sandpaper and coated-abrasive applications require written material-manufacturer approval and tests of the backing, binder and fumes. Epoxy, phenolic or halogen-containing products must not be treated as generic laser-safe abrasives. A larger bed or skew-correction feeder is a separately confirmed option.
Configuration and specifications
| Parameter | Product configuration |
|---|---|
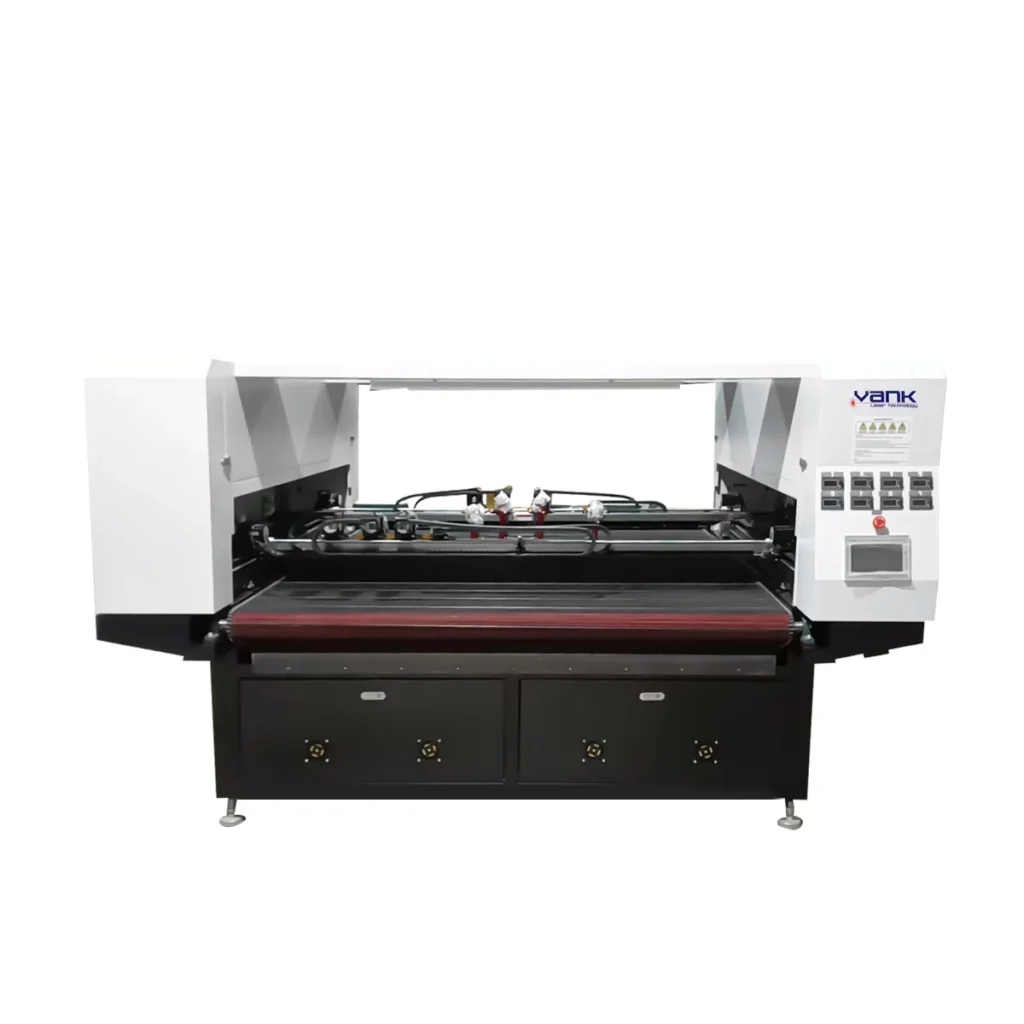
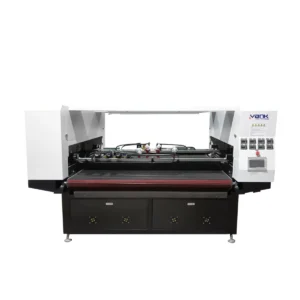
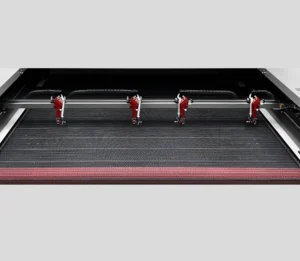
| Model / format | VankCut-1812 eight-head |
| Nominal working area | 1800 × 1200 mm |
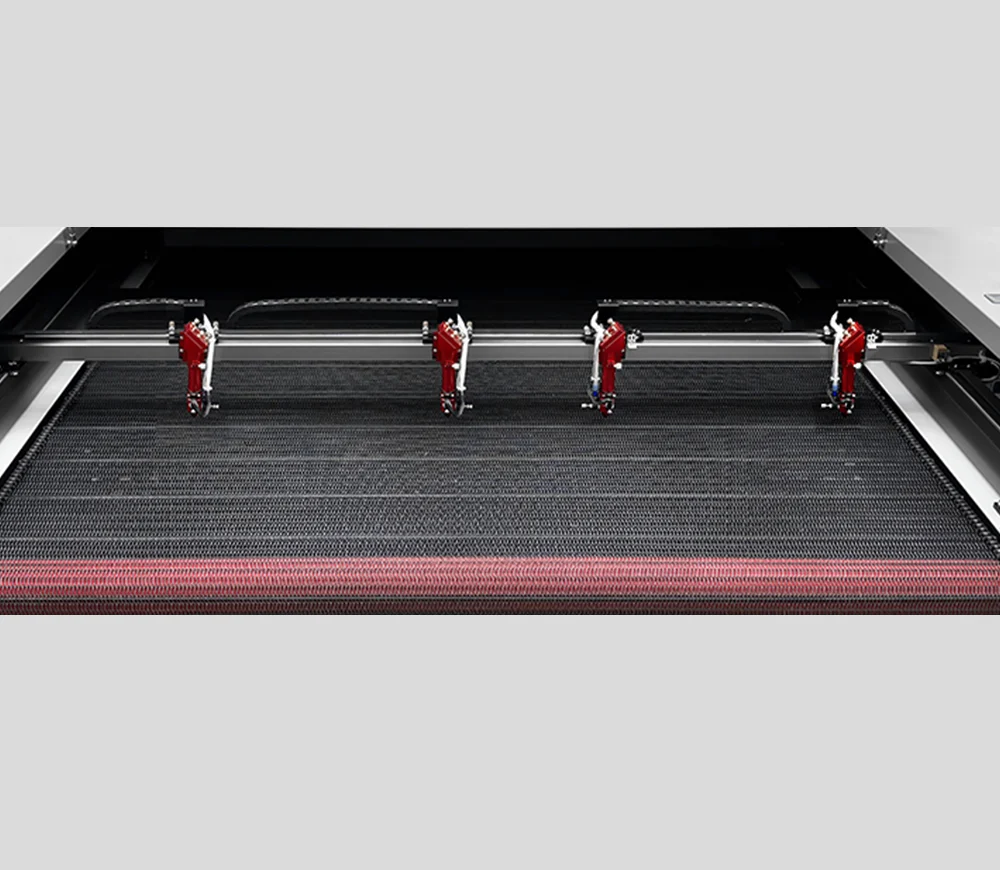
| Cutting heads | 8 |
| Laser power options | 100 / 120 / 150 / 180 / 200 W classes; per-head power and tube count specified |
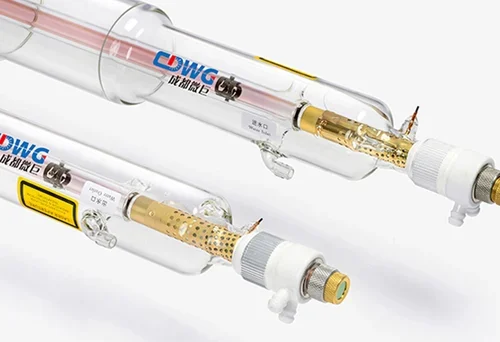
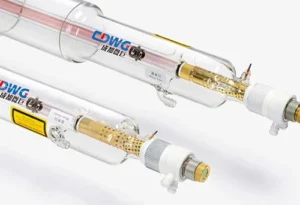
| Laser source | Water-cooled sealed CO2 glass tube |
| Nominal wavelength | 10.6 µm |
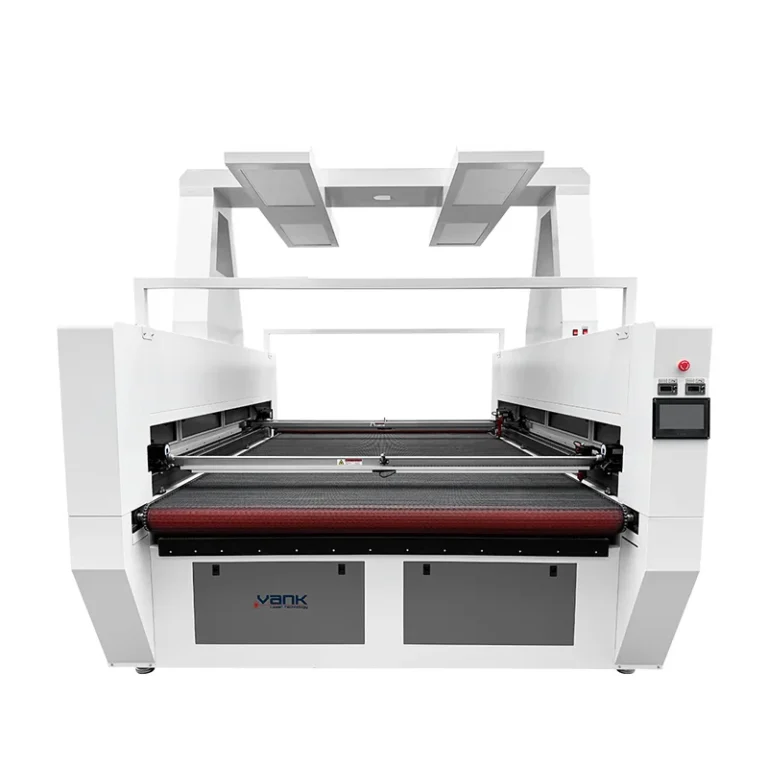
| Material feeding | Indexed conveyor with automatic roll feeder |
| Vision system | Camera configuration confirmed with printed sample |
| Controller / software | Trocen TL5269 multi-head configuration |
| Cooling | Industrial water chiller matched to source power |
The values below identify this product and its listed options. The selected source, optics, controller, accessories and site utilities must be named in the quotation. Motion speed and positioning figures do not establish finished-part tolerance or production throughput.
Materials and process limits
Typical textile trials include polyester sportswear, nylon, cotton, denim, felt, lace, embroidery and identified nonwovens. Thermoplastic fibers may form sealed edges; natural fibers can char or fray. Check dyes, coatings, backing and adhesives before testing. Safety-critical or protective textile products require separate process validation.
Identify the exact material, coating and adhesive before testing. Do not laser-process PVC, vinyl, PTFE, other halogen-containing materials or unidentified composites. Use material-specific extraction and continuous supervision during cutting.
Production workflow
Load the roll, set tension and align the feeder with the conveyor. For plain fabric, import and nest the cutting file. For vision-equipped models, calibrate the camera, capture the print or embroidery and review the generated contours. Cut a sample, inspect edge and dimensions, then verify indexing across successive feed sections.
Options to specify
Specify roll width, diameter, weight, stretch and print repeat. Head spacing and synchronous or independent motion determine which layouts can run together. Camera field, lighting, edge guidance, chiller capacity, per-head air assist and extraction must suit the complete configuration. Extra heads do not automatically multiply output by the head count.
Plan suitable guarding, interlocks, emergency stops, extraction and operator training for the supplied laser system. The finished machine classification must be verified; an enclosure alone is not proof of Class 1 compliance. Follow the supplied operating and maintenance instructions.
Sample test and acceptance
Approve a representative sample and the written configuration before ordering. Record the material, source, settings, lens or nozzle, fixture, appearance, dimensions and complete cycle time. Keep those results as the production acceptance reference.
Camera recognition limits
Recognition depends on print contrast, lighting, stretch, distortion, camera calibration and the supplied software. Use actual printed rolls to measure contour error, missed detections, edge quality and complete cycle time, including feeding and unloading. Plain-fabric models require an explicitly included vision option for this workflow.
Installation, service and documentation
Ask Vank Laser to include the machine layout, electrical requirements, supplied software, operating instructions, maintenance schedule and recommended spare parts in the technical proposal. Agree commissioning, operator training, support language, warranty coverage and service responsibilities before shipment. Request conformity documents for the actual machine and destination.
Request a sample test and quotation
Send the fabric composition, coating or backing, roll dimensions and weight, artwork or printed sample, head-count preference, contour tolerance and daily output target.
Send the destination country, installation voltage and required delivery scope with your inquiry. Ask for sample photos or video, measured results and a configuration-specific quotation.
Request a sample test and configuration quote
Compare related machines
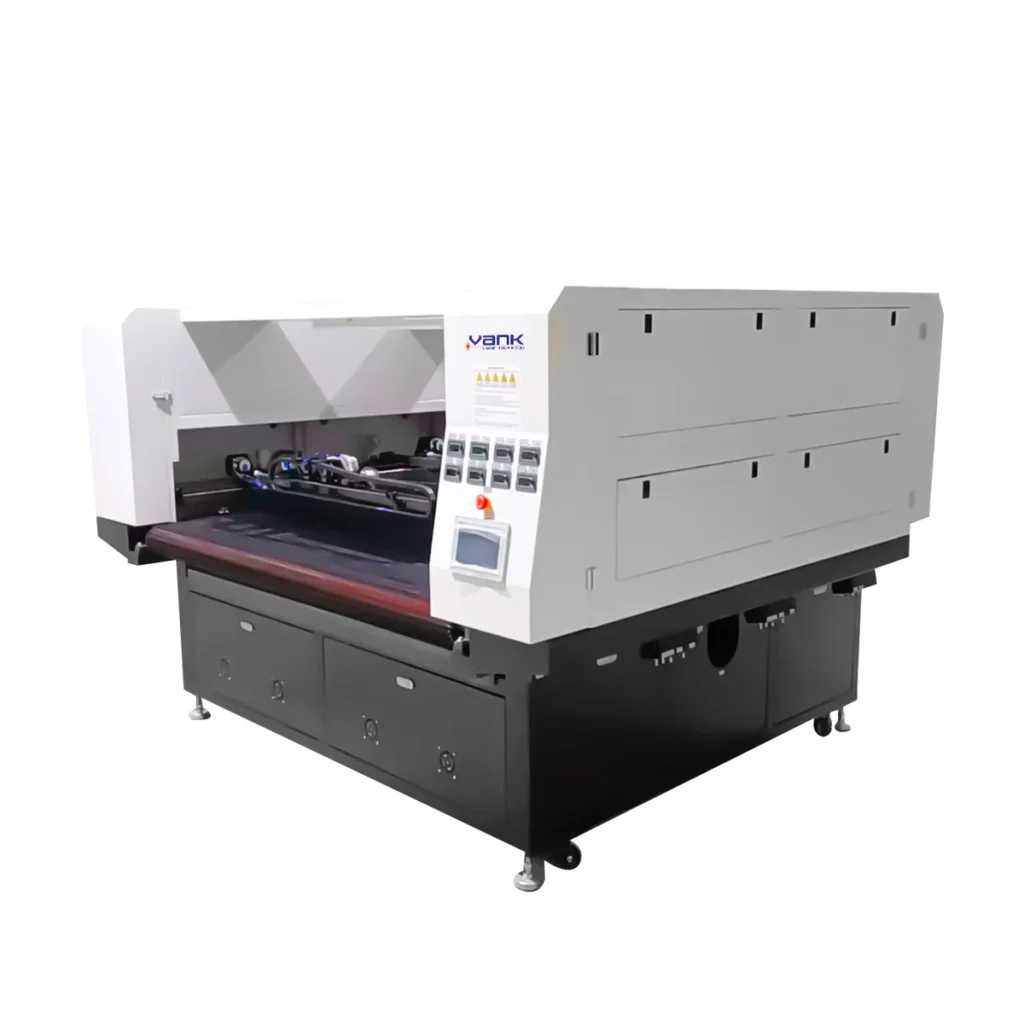
Machine and component photos
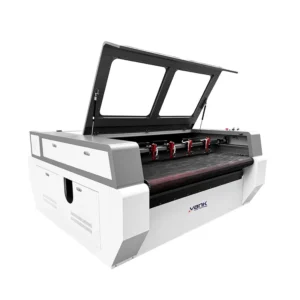
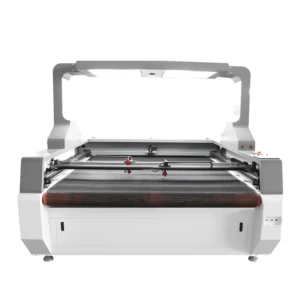
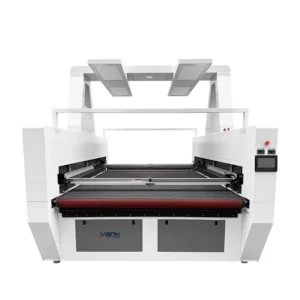
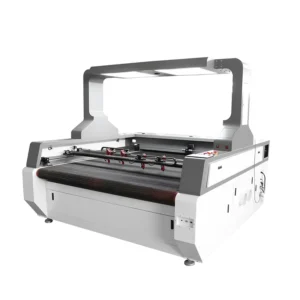
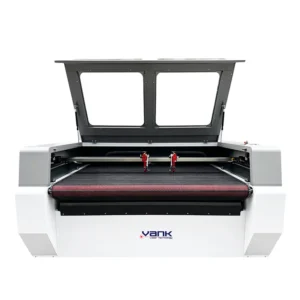
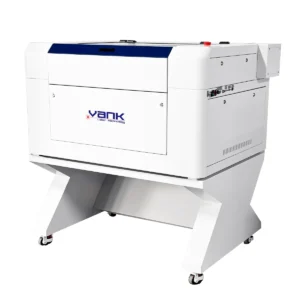
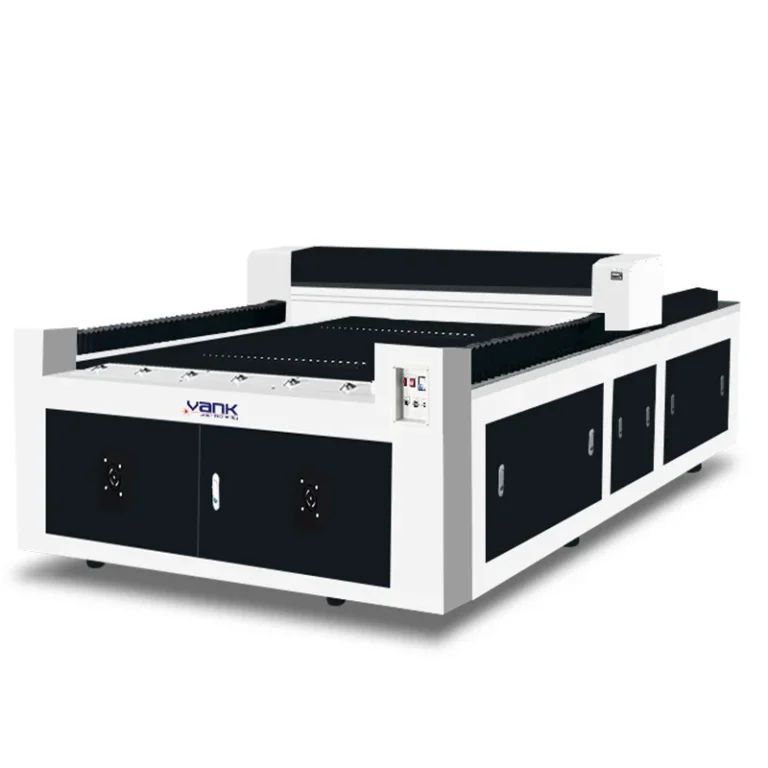
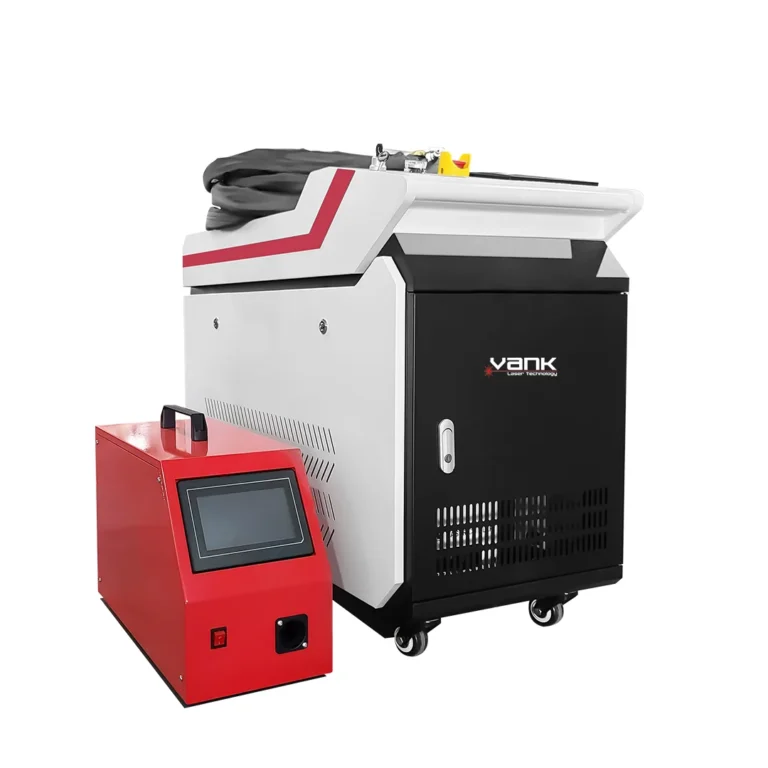
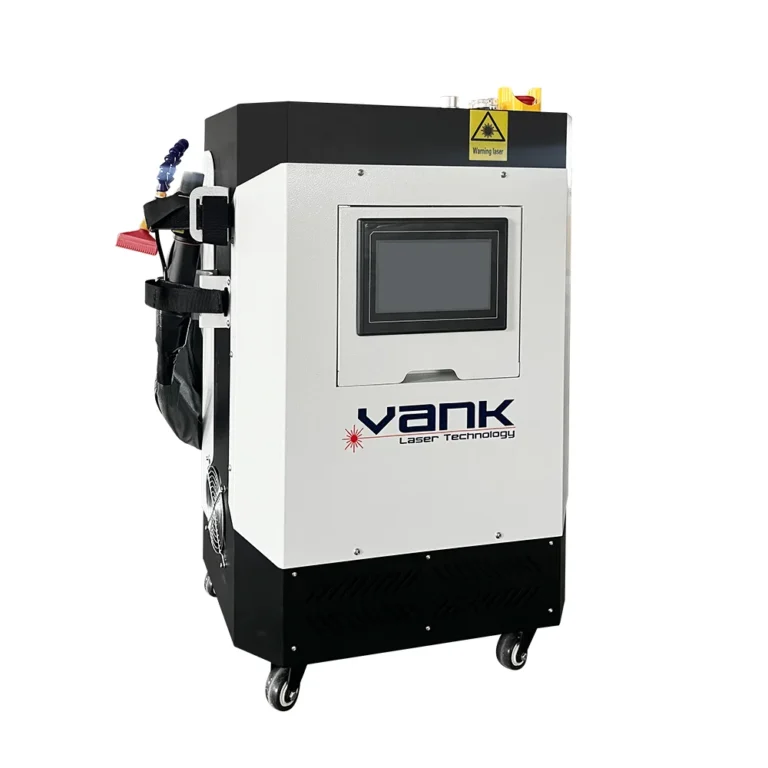
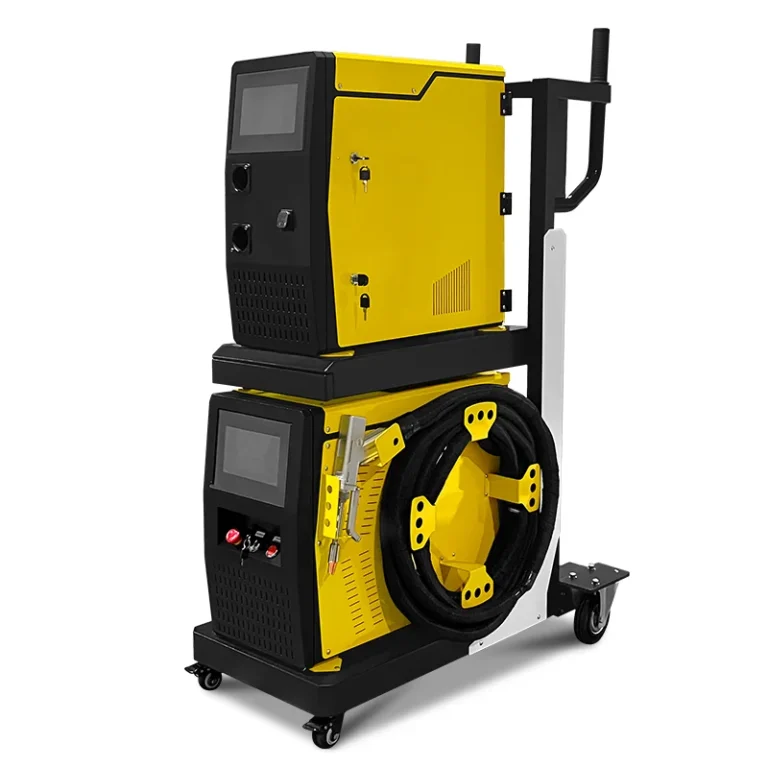
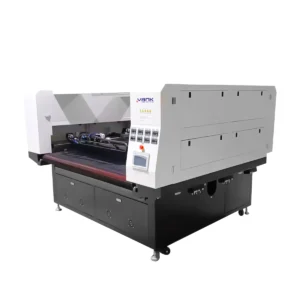
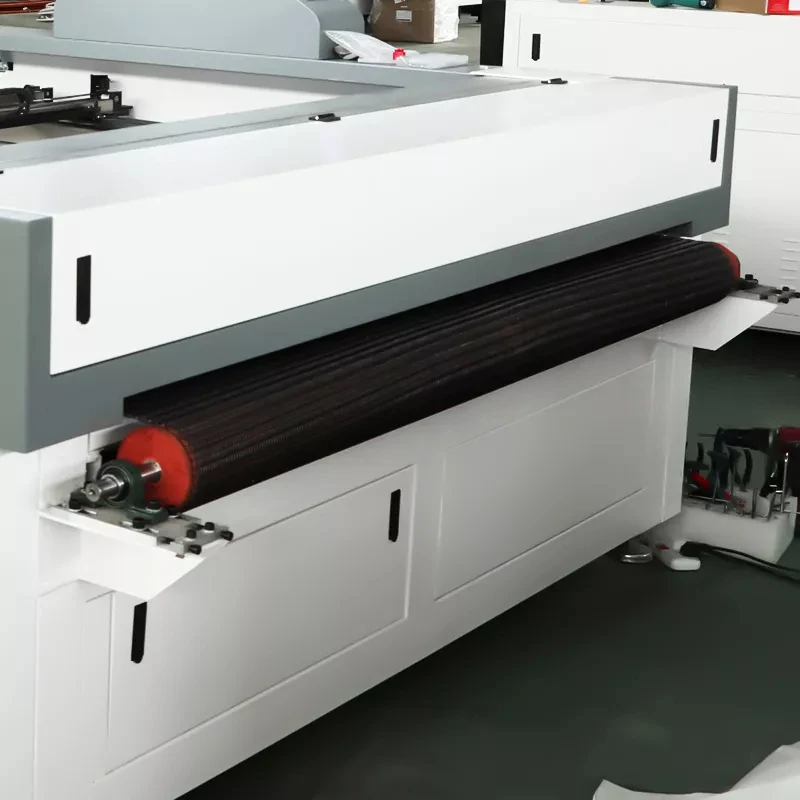
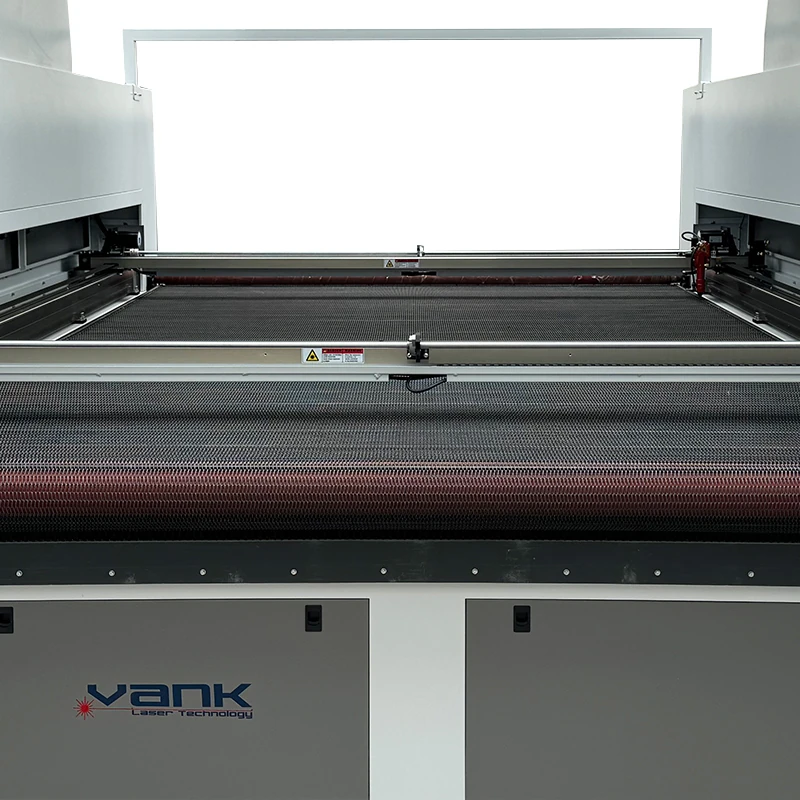
Photos illustrate the product or component family. Included brands, accessories and configuration are defined in the approved quotation.
Product videos
Vank product-family demonstration. The machine shown may have a different power or optional equipment; confirm the configuration for your order.